
RO Membrane Production Line Suppliers: Seven Checks Before You Buy
How to verify the people, process and acceptance evidence behind a machine proposal.
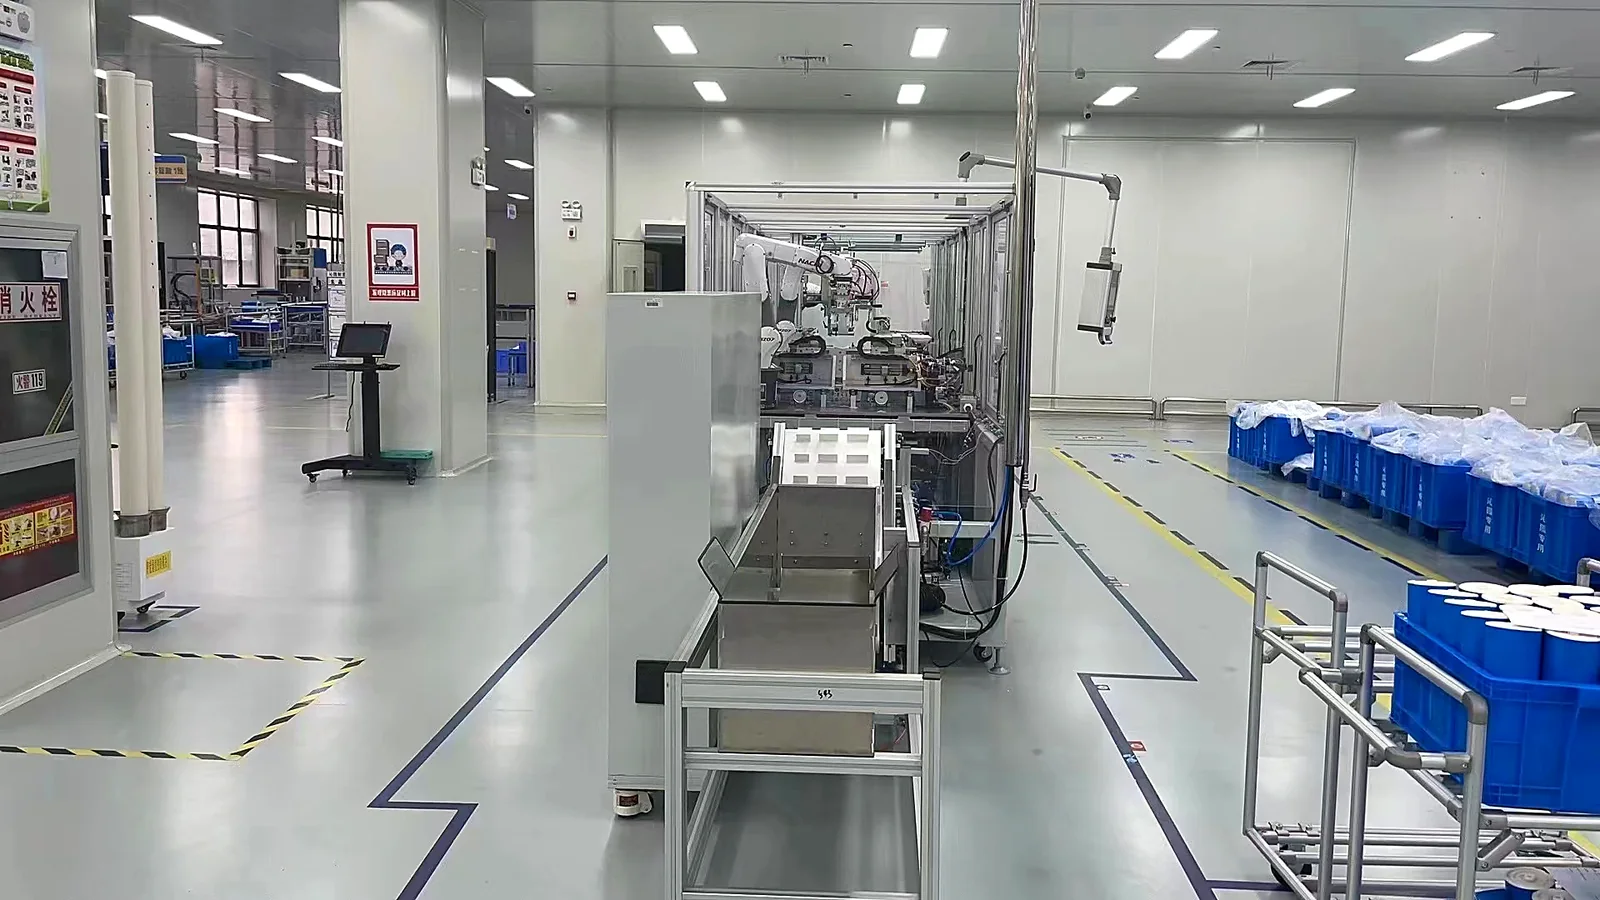
Direct answer: choose a production-line supplier on documented delivery scope, not an equipment list alone. Verify the element recipe, machine interfaces, FAT/SAT criteria, training, site utilities, traceable sample output and responsibility after installation. A quotation without these items is not yet comparable with a commissioned line proposal.
A plant making 1812 household elements and one making 4040 or 8040 industrial elements do not need the same tooling, materials or acceptance test. This article focuses on auditing a supplier’s delivery claims. For the separate question of which stations a line requires, see our production-line checklist.
Seven Checks for a Production-Line Supplier
Element drawing and process boundary
Send the target size, membrane leaf design, material starting state and finished-element requirement. Ask where the quoted line begins and ends.
Station-by-station responsibility
Mark cutting, carrier preparation, adhesive application, rolling, curing, trimming, wrapping, vacuum test and final QC as included, optional or buyer-supplied.
Material-to-machine compatibility
Test actual sheet, feed spacer, carrier, tube and adhesive samples on the quoted tooling. A similar catalog grade is not an approved production recipe.
Output basis
Request good elements per shift, operator count, changeover assumptions and first-pass yield. Separate demonstrated station speed from balanced line output.
Factory acceptance test
Agree on FAT samples, format changes, safety checks, dimension checks and recorded test results before shipment.
Site acceptance and training
List power, air, test water, space, installation days, operator training and the person responsible for solving process problems on site.
Support after handover
Record spare-parts lead time, remote support, documentation language, warranty boundary and the process for recipe changes.
Make FAT and SAT Meaningful
FAT is performed before shipment under agreed conditions; SAT checks the delivered equipment at the buyer’s site. Neither should be reduced to “machine powered on”. Specify the element format, approved material lots, operator involvement, sample quantity, cycle-time definition and pass/fail records. If a line includes a vacuum testing station, define what that station screens and how rejects are investigated; a vacuum test is not a substitute for every performance test.
| Record | Minimum buyer question | Common gap |
|---|---|---|
| Line layout | Can materials, operators, rejects and finished elements move without cross-traffic? | A CAD layout without utility or access clearances |
| Sample build | Were the samples built from approved materials and the target element drawing? | Demonstration with easier substitute materials |
| Cycle-time log | Does timing include loading, glue, unloading and normal operator actions? | One isolated machine-motion figure |
| QC report | Which dimensions, leak checks and performance tests were recorded? | Pass/fail statement without method or conditions |
| Training record | Who can set up, run, clean and troubleshoot the line after handover? | No named trainees or sign-off |
What an On-Site Case Can and Cannot Prove
WECOME’s published Payas India account describes on-site support for a customer’s 4040/8040 RO element manufacturing project, including equipment placement, commissioning, process setup and operator training. It is evidence of that documented support role. It is not proof that Payas purchased every machine shown on the WECOME site, nor a universal output guarantee for other factories.
Read the Payas India on-site support case and our technical support scope.

Compare Suppliers on the Same Basis
Put every offer into one comparison table with the same rows: element size, approved recipe, station boundary, expected good output, buyer utilities, FAT, SAT, training, spares and exclusions. Do not mark an item as “included” because it appears in a marketing image. Confirm its model, quantity and responsibility in the signed scope.
Buyers comparing individual machines can use our rolling-machine selection guide. For project budgeting, the production-line cost guide explains why a cheap equipment subtotal can become an expensive factory project.
Supplier Audit FAQ
What is the difference between an equipment vendor and a line integrator?
An equipment vendor may supply one or more machines. A line integrator is responsible for defined interfaces between stations and may support layout, installation, commissioning and acceptance. The contract, not the label, determines the actual responsibility.
Should I visit the supplier before placing an order?
A visit or live witnessed trial can be valuable for a large project, but it should follow a written technical brief. Ask to see the quoted model, a relevant element build and records for the same process boundary.
Does a case study replace FAT or SAT?
No. A case study illustrates previous work. FAT and SAT establish whether the equipment and process supplied for your specific project meet agreed acceptance criteria.
Review Your Line Scope With WECOME
Send your element format, current or target material stack, output requirement, workshop utility information and preferred support boundary. We can identify the machines and verification steps that belong in a comparable proposal.
Discuss a Production LineScope and source note
This is WECOME’s practical supplier-evaluation framework, not an independent ranking. The Payas example is limited to the role described in WECOME’s published case. Confirm project-specific contractual and technical details before ordering.

Bessie has 10+ years of experience in RO membrane materials and water treatment supply chains. At WECOME, she helps manufacturers and system integrators worldwide source the right membrane components — from feed spacers and permeate carriers to NSF-certified adhesives — backed by hands-on technical support.